Menu
Close
Choosing the right Plastic Extruder starts with the material and product, not the machine’s headline output. A line designed for flexible film may not suit rigid pipe or a precise profile. Resin type, additives, moisture sensitivity, and recycled-content variation can all affect processing. Small details matter. A color change, for example, may require more purging time than expected.
Compare the required output with the extruder’s stable operating range. Ask about screw design, diameter, and length-to-diameter ratio, then check whether temperature zones can hold steady during a production run. A neat control panel is useful, but it cannot compensate for a poor match between screw and material. Request trial data using a representative resin, and look closely at melt quality, output consistency, and energy use. Numbers from a brochure are only a starting point.
The extruder is also part of a line. Its die, screen changer, cooling system, haul-off, and controls must work together. Consider available floor space, operator experience, cleaning access, spare parts, and service response. These practical limits are easy to overlook when comparing specifications. I would not assume the largest machine is the safest investment; oversized equipment can run inefficiently at low output. Nor is the lowest purchase price always economical. The right choice depends on verified production needs, realistic growth plans, and support you can actually reach. Some uncertainty remains until a material is tested on the machine. That is worth admitting before placing an order.
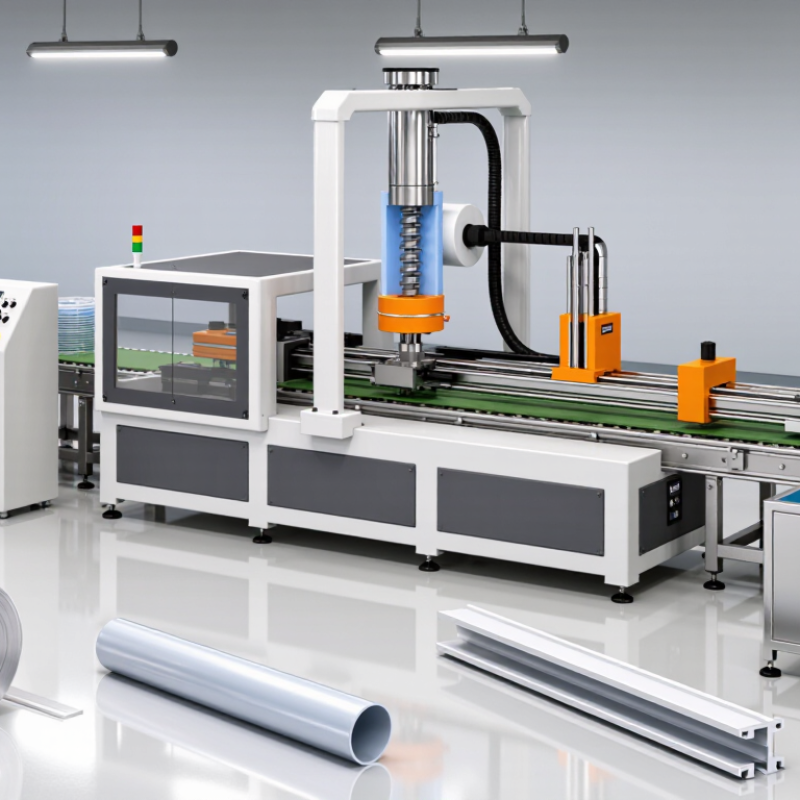
The right extruder starts with a precise description of the material. “Polyethylene” alone is not enough. Identify the resin grade, melt-flow range, additives, fillers, and recycled content. These details affect screw design, barrel temperature, and wear. Check the supplier’s technical data sheet, but verify key values with incoming-material tests when consistency matters. Small differences can change how steadily the melt flows.
Moisture and heat sensitivity deserve attention. Some polymers need drying before processing; others can degrade if they remain too hot for too long. Note the recommended processing window and any special handling requirements. It is tempting to specify only the resin family. That is often too vague. In practice, a damp pellet or a changing recycled blend can cause bubbles, surface marks, or unstable output. A trial run may reveal problems that a data sheet cannot.
Describe the finished product just as carefully. Record its shape, dimensions, wall thickness, tolerance, and expected output per hour. A thin tube, for example, needs different flow control and cooling than a thick sheet. Include the die and downstream equipment in the discussion; an extruder cannot compensate for every design mismatch. Define acceptable variation, too. Exact targets help, but real production has limits. Leave room to review samples and adjust settings before committing to a full production run.
Start with the resin grade and the finished product’s dimensions, tolerances, output, and end-use requirements. Processing temperatures and drying conditions are typical starting points; confirm them with the resin supplier and conduct trials for the selected grade and equipment.
| Plastic material | Common extruded products | Typical melt-processing range | Drying considerations | Extruder and process considerations | Product specifications to define |
|---|---|---|---|---|---|
| HDPE High-density polyethylene | Pipes, sheets, profiles, film, and blow-molding parisons | Approximately 180–230°C, depending on grade and product | Usually not required for properly stored, standard grades; remove surface moisture if present. | A general-purpose single-screw extruder is common. Select screw design, die, and cooling system for the product and output rate; control melt temperature and pressure. | Pipe diameter and wall thickness; profile dimensions; sheet thickness; dimensional tolerance; output rate; pressure or impact requirements. |
| PP Polypropylene | Strapping, sheets, profiles, pipes, and fibers | Approximately 190–240°C, depending on grade and product | Typically no predrying is needed for standard grades if the resin is kept dry and clean; follow grade-specific instructions. | Use a screw and die suited to the grade’s melt flow and product geometry. For fibers or thin products, stable throughput and precise cooling are important. | Width, thickness, tensile properties, shrinkage, surface finish, line speed, and intended service temperature. |
| PVC Rigid or flexible compounds | Pipes, window profiles, cable insulation, tubing, and sheets | Often approximately 160–200°C; the compound and process window are critical. | Usually not required for dry compound; protect material from moisture and contamination. | Choose a PVC-compatible screw, barrel, and temperature-control system. Limit excessive heat and residence time to reduce degradation; confirm materials of construction and venting needs with the equipment supplier. | Rigid or flexible formulation; profile geometry; wall thickness; dimensional tolerance; surface quality; required standards and application conditions. |
| PET Polyethylene terephthalate | Sheet, film, strapping, and monofilament | Often approximately 260–290°C, depending on resin grade and application | Thorough dehumidifying drying is generally essential. Temperature, time, and target moisture depend on the grade; excessive moisture can cause hydrolytic degradation during processing. | Consider a dehumidifying dryer, moisture measurement, controlled feeding, and a melt system designed for the required output and product. Manage residence time and avoid contamination. | Sheet or film thickness, width, optical clarity, moisture-sensitive quality requirements, tensile properties, and production rate. |
| ABS Acrylonitrile butadiene styrene | Profiles, sheets, pipes, and appliance or automotive trim | Approximately 200–250°C, depending on grade and product | Often requires predrying because absorbed moisture can cause surface defects; use the resin supplier’s specified drying conditions. | Match screw design and output to the grade’s melt flow and product dimensions. Stable melt temperature and effective calibration or cooling help maintain dimensional accuracy. | Impact strength, surface finish, color, profile or sheet dimensions, tolerance, and any required flame or weathering performance. |
| LDPE / LLDPE Low-density polyethylene grades | Blown film, cast film, tubing, and coatings | Approximately 160–230°C, depending on grade and process | Typically not required for standard grades if stored correctly; prevent moisture and foreign-material contamination. | For film, consider a film screw, die design, cooling capacity, and haul-off system. Match die width and line speed to target film width, gauge, and output. | Film width and thickness, lay-flat width, bubble stability, optical properties, sealability, and line output. |