Choosing the right Liner Plate Material is not a simple matter of picking the hardest option. In a ball mill, crusher, chute, or hopper, the plate faces a different combination of impact, abrasion, heat, and corrosion. A material that performs well in dry limestone may fail quickly in wet, acidic ore. Small details matter. Feed size, drop height, operating temperature, and maintenance access can change the result. The best choice begins with actual service conditions, not a supplier’s generic product label.
Experienced maintenance teams usually compare abrasion resistance with toughness. High-chrome white iron can resist sliding wear, yet severe impact may cause cracking. Alloy steel often tolerates repeated impact, while rubber can reduce noise and protect against certain corrosive slurries. Ceramic liners may deliver exceptional hardness, but installation quality and support conditions remain critical. These trade-offs should be checked against test data, operating records, and recognized material standards. Ask suppliers for chemical composition, hardness ranges, impact values, recommended thickness, and documented applications. Unclear claims deserve careful questions.
A reliable selection process also considers total cost, not only purchase price. A cheaper plate can create frequent shutdowns, difficult replacement work, and unexpected production losses. Measure wear patterns during inspections and record service life under comparable conditions. Then revise the specification when evidence contradicts assumptions. No selection is perfect. Even a carefully engineered liner can underperform if bolt tension, alignment, or feed control is poor. This guide explains how to compare options realistically, communicate requirements clearly, and choose a Liner Plate Material with defensible performance expectations.
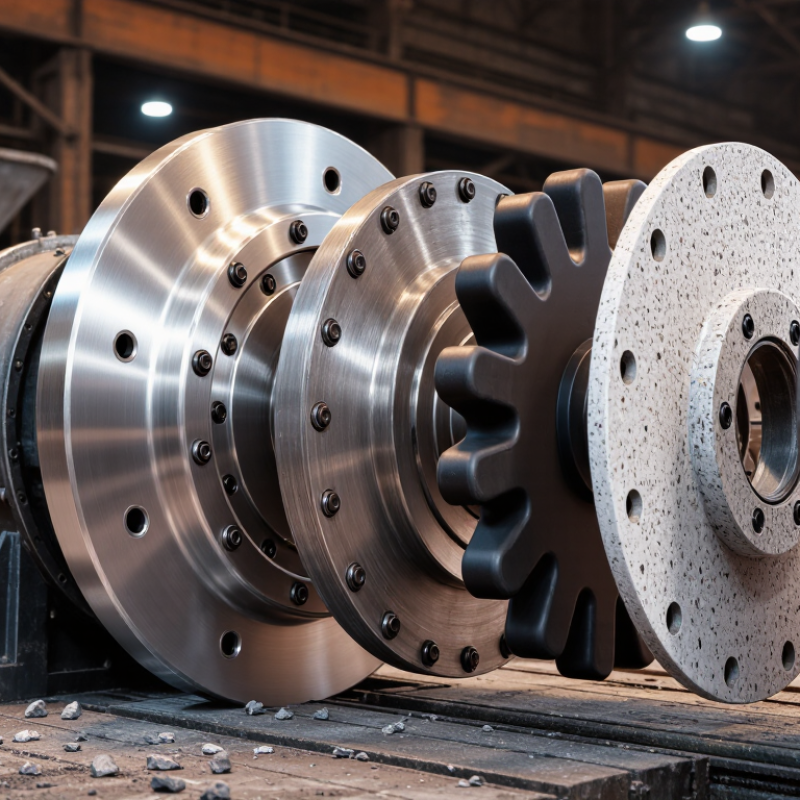
A liner plate is a replaceable protective layer inside mills, chutes, hoppers, and crushers. It absorbs impact and shields the equipment shell from abrasive ore. Its material matters because wear changes operating cost, maintenance time, and worker exposure to repair conditions. The World Steel Association reported 1.89 billion tonnes of crude steel production in 2023. That scale reflects the severe duty placed on mineral-processing equipment worldwide.
Material selection should match the failure mechanism. High-chromium white iron often suits sliding abrasion, while manganese steel can work better under heavy impact. Rubber and composite liners may reduce noise and weight, but they can struggle with sharp, hot, or oversized feed. ASTM G65 testing compares abrasive wear resistance, yet laboratory results cannot fully reproduce a wet mill or uneven feed stream. Hardness alone misleads.
In field inspections, I would record feed size, moisture, impact height, temperature, and actual wear depth. A plate that lasts longer may still be unsuitable if installation takes twice as long. The 2024 USGS Mineral Commodity Summaries describe continued global demand for iron ore, copper, and other mined materials, reinforcing the need for durable protection in continuous processing circuits. Still, published data must be read carefully. Test media, pressure, and failure definitions differ between studies. A practical choice combines ASTM test results, site measurements, and maintenance records, rather than relying on a single impressive number.
Liner plate selection should begin with the working environment, not a material catalogue. Abrasive feed can wear steel quickly when particles are sharp, hard, or continuously recycled. Large rocks create impact damage, while fine particles create steady sliding wear. These actions may occur together. The difference matters.
Temperature, moisture, and chemical exposure also change performance. Heat can reduce hardness or distort a liner under load. Water may accelerate corrosion, especially when contaminants remain trapped against the surface. In a wet mill, a corrosion-resistant alloy may outperform a harder material. In a dry chute, impact resistance may matter more. I have seen similar equipment require different liners because operating habits changed. Laboratory data helps, but field conditions can be less predictable.
Tips: Record feed size, hardness, moisture, temperature, impact energy, and replacement intervals. Inspect worn liners closely. Uneven grooves may indicate poor material matching or incorrect installation. Ask whether downtime costs more than a higher initial price. A practical trial is often useful. Still, one trial does not prove everything. Review the results after several operating cycles, and question unexpected wear patterns. Also check bolt condition, support gaps, and alignment. These details are easy to overlook. They can make a good material appear unsuitable.
Choosing liner plate material requires more than comparing hardness values. ASTM A128 manganese steel commonly enters service near 200–250 HB. Under heavy impact, its surface can work-harden beyond 500 HB. This makes it suitable for large rocks and changing feed sizes. It can perform poorly, however, in low-impact sliding wear. The World Steel Association reported nearly 1.9 billion tonnes of crude steel production in 2024, showing steel remains widely available. Availability does not guarantee the right performance.
High-chromium white iron, covered by ASTM A532, often reaches approximately 550–750 HB. It resists fine-particle abrasion better than manganese steel. It is also more brittle. A sudden tramp-metal event may create cracks or broken sections. Rubber liners usually measure about 60–80 Shore A, based on ASTM D2240 practices. They reduce noise and absorb impact. Their weakness appears with sharp, hot, or chemically aggressive material.
Ceramic inserts can exceed 1,500 HV, while polyurethane commonly falls near 80–95 Shore A. These materials suit severe sliding wear or lighter-duty impact zones. Field inspections often show mixed conditions inside one mill. One area may need abrasion resistance, while another needs flexibility. A hardness chart can mislead. Review feed size, impact energy, moisture, temperature, and shutdown records before selecting a material. The wrong choice may last longer on paper but fail earlier in service.
How to Choose the Right Liner Plate Material?
Wear resistance should be measured against the actual material flow, not a catalog hardness value. In a quarry, sharp quartz particles can cut the surface like glass. In a coal chute, softer particles may cause slower, sliding abrasion. Inspect the worn liner and record thickness loss, feed size, flow speed, and service hours. A simple wear-rate calculation often reveals more than a single hardness test.
Impact resistance needs a different evaluation. Watch where rocks strike, how high they fall, and whether the liner flexes or cracks. A very hard plate may resist scratching but fracture under repeated blows. Check impact-test results, weldability, and crack patterns after operation. Small edge cracks deserve attention. They can grow beneath apparently sound surfaces.
Corrosion resistance depends on moisture, chemicals, temperature, and cleaning practices. Measure surface pH when possible, and examine pits rather than only general rust. Salt water, acidic slurry, and trapped deposits may create localized attack. Laboratory immersion tests help, but field coupons are more realistic. I have seen material selections fail because corrosion was treated as secondary. That judgment needs reconsideration. The best choice balances hardness, toughness, corrosion performance, thickness, and replacement access for the full operating environment.
Indicative material comparison based on commonly published typical engineering ranges; final selection should be verified against project-specific test data and material specifications.
How to Choose the Right Liner Plate Material?
Cost, maintenance, and service life should be judged together, not separately. A low-priced liner may reduce the purchase budget, but frequent replacement can increase labor, shutdown, and disposal costs. In a busy crushing circuit, even a few extra hours of downtime can outweigh the initial saving.
Start with the operating conditions. Measure feed size, impact force, sliding abrasion, temperature, and moisture. A hard material can resist wear, but it may crack under heavy impact. A tougher alloy may survive impacts longer, although it can wear faster in constant sliding contact. Maintenance records are useful here. Check which zones fail first, how quickly cracks appear, and whether bolts or edges need repeated adjustment.
Service life should include installation effort. A liner lasting twelve months is not automatically better than one lasting eight months. The longer-lasting option may require special lifting equipment, longer lead times, or difficult fitting. Those details matter. Ask for verified test data and compare it with your own operating history. Laboratory results can be helpful, but they rarely copy every site condition. An honest calculation should include uncertainty, because wear rates can change after feed characteristics change. The cheapest decision is sometimes reasonable. Not always.
Comparative planning guide for common liner materials used in mills, chutes, hoppers, bins, and transfer points.
| Liner Material | Typical Material Cost (USD/m²) | Typical Service Life (Months) | Maintenance Profile | Abrasion Resistance | Impact Resistance | Operating Temperature | Best-Fit Applications |
|---|---|---|---|---|---|---|---|
| Natural Rubber Flexible Low noise | Low $40–$120 | 3–12 | Generally simple to install and replace. Requires more frequent thickness checks in highly abrasive zones. | Good for wet, coarse, and moderately abrasive material; less suitable for sharp, dry particles. | Excellent Absorbs impact and reduces rebound. | Approximately −50°C to 80°C | Wet chutes, screens, bins, and impact zones where noise reduction is important. |
| Polyurethane Lightweight Wet service | Low to medium $80–$220 | 4–18 | Low maintenance when correctly fitted. Regular inspection is needed for cutting, tearing, and edge lifting. | Very good against fine wet abrasion and sliding wear; performance depends strongly on formulation. | Good Moderate impact absorption. | Approximately −40°C to 90°C | Fine ore, sand, slurry-related handling, screens, and applications requiring low weight. |
| Manganese Steel High impact Work-hardening | Medium $120–$300 | 6–24 | Robust and repairable, but heavy. Bolt and fastening checks are important because loose hardware can accelerate damage. | Good under impact; wear resistance improves when the surface work-hardens under suitable loading. | Excellent Preferred for severe impact and large feed size. | Approximately −40°C to 300°C | Primary crushers, large-rock chutes, dump pockets, and heavy-impact loading areas. |
| High-Chromium White Iron High abrasion resistance Hard surface | Medium to high $180–$450 | 9–30 | Longer replacement intervals in sliding-abrasion service. Brittle sections require careful handling and correct support. | Excellent against dry sliding abrasion and fine-to-medium abrasive particles. | Limited to moderate; may crack under severe impact or installation shock. | Approximately −40°C to 500°C | Chutes, mill discharge areas, separators, and dry abrasive handling with controlled impact. |
| Ceramic-Backed Composite Longest wear life Low weight options | High $250–$700 | 12–36 | Higher installation cost and stricter bonding or fastening requirements. Planned inspection is still necessary around joints and edges. | Excellent for severe sliding abrasion and high-throughput material flow. | Moderate; rubber-backed designs tolerate more impact than rigid ceramic-only designs. | Approximately −30°C to 120°C for bonded systems | Transfer chutes, high-wear bends, pulverized material handling, and areas with costly downtime. |
We offer Packaging Boxes delivered to your door. Secure, professional, and affordable, our custom made packaging boxes are guaranteed to protect and transport your valuable items. Our devoted team is always there to serve you.