Menu
Close
Choosing a Cnc Precision Machining supplier can shape part quality, delivery reliability, and the true cost of a project. A low quote may look attractive, but it tells only part of the story. The useful questions concern capability, inspection, communication, and how the supplier handles changes. Details matter.
A drawing may specify tight tolerances, a fine surface finish, or a critical hole position. Ask how these features will be measured, what inspection records are available, and whether the supplier has made comparable parts. Where possible, review a representative sample or discuss a first-article inspection before releasing a larger order. Specific answers build confidence. Vague promises do not.
This guide explores practical ways to assess machining equipment, materials expertise, quality systems, lead times, and customer support. It also considers whether a supplier can scale from prototypes to repeat production without losing consistency. Certifications can provide useful evidence, but they should not replace questions about actual processes and results. A polished presentation is not proof.
There is no single checklist that fits every component. A simple bracket and a complex medical-device housing demand different controls, and buyers should reflect on which risks matter most. The right supplier is not automatically the largest or cheapest. It is the one whose capabilities, evidence, and working style match the part—and who can explain limitations before they become surprises.
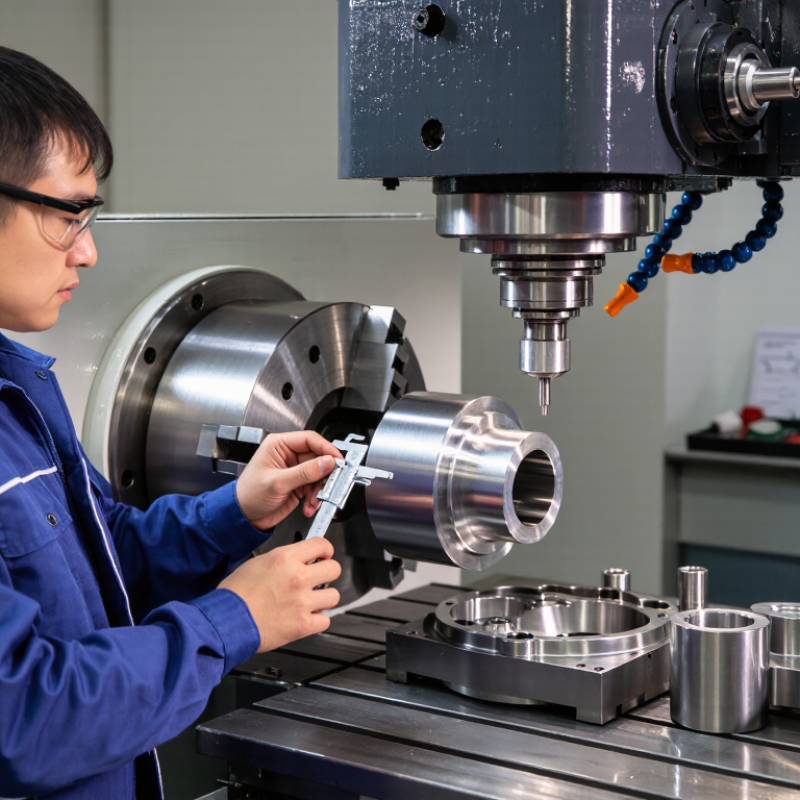
A CNC supplier can only quote accurately when the drawing defines what matters. Specify datums, feature control frames, and inspection points using GD&T. A hole pattern may need a true-position tolerance relative to two mounting faces, not just a location dimension. Small details matter.
Use ISO 286 fits when mating parts need a predictable clearance or interference. For a shaft and bore, state the nominal size and fit class, such as H7/g6, rather than writing “close fit.” Confirm the material, process, and inspection method with the supplier. A fit that works in aluminum may behave differently in steel, especially when temperature or surface finish changes. I have seen drawings leave this unstated; it can lead to avoidable rework.
Ask how the supplier verifies critical features. A coordinate measuring machine may suit a complex position tolerance, while calibrated bore gauges can check repeated diameters efficiently. Request sample inspection results and ask whether measurement uncertainty is considered near tolerance limits. Also check that the datum setup matches the part’s real assembly condition. A beautiful report is less useful if the fixture references the wrong surface. Some requirements may still need discussion before release.
| Requirement Area | Example Part Requirement | GD&T or Fit Definition | What to Confirm with the Supplier | Suitable Verification Evidence |
|---|---|---|---|---|
| Drawing and revision control | Machine to the released 2D drawing and 3D model; identify the governing document and revision. | Specify applicable drawing units, general tolerances, datums, and any model-based definition requirements. | Can the supplier review the full drawing package, identify ambiguous dimensions, and control revisions through production? | Documented drawing review, revision identification on the job traveler, and approval of clarified requirements before machining. |
| Datum reference frame | Locate a mounting face as primary datum A, a locating bore axis as datum B, and a side face as datum C. | Use datum references in feature control frames where the functional relationship requires them. | Does the inspection method establish the same datum reference frame used to define the part’s function? | Inspection plan showing datum setup, measurement alignment, and the features checked relative to A, B, and C. |
| Position of holes | Example: a pattern of four clearance holes located from the mounting face and two locating features. | Define a position tolerance with a diameter symbol and the applicable datum references; state the tolerance value on the drawing. | Can the supplier hold and measure the stated position tolerance using a method suitable for the part size and tolerance? | CMM report or other traceable measurement record listing actual hole locations and the evaluated position tolerance. |
| Flatness of a sealing face | Example: control the flatness of a machined sealing surface where contact across the surface is functionally important. | Specify a flatness tolerance on the surface; flatness is a form control and does not use a datum reference. | Can the supplier select a measurement approach that represents the surface condition and stated tolerance? | Surface measurement results from an appropriate instrument or documented inspection method, with the measurement area identified. |
| Perpendicularity of a bore axis | Example: keep a bore axis perpendicular to a mounting face used as a functional reference. | Apply a perpendicularity control to the axis and reference the relevant datum plane, such as datum A. | Will the supplier inspect the axis relative to the specified datum rather than checking only the bore diameter? | Measurement report showing the bore axis orientation relative to the datum setup. |
| Hole-and-shaft fit | Example: a rotating shaft in a housing bore where a clearance fit is required. | Specify a fit such as H7/g6 when appropriate. ISO 286 fit limits depend on the nominal size and the specified tolerance grades. | Can the supplier manufacture and inspect both mating features to the selected limits, including any required surface finish? | Actual bore and shaft measurements, material or process records where required, and confirmation against the applicable ISO 286 size range. |
| Close-clearance or location fit | Example: a removable locating component requiring small clearance for assembly and repeatable positioning. | A fit such as H7/h6 may be considered, subject to functional analysis and the applicable nominal-size limits in ISO 286. | Does the supplier understand whether the fit is intended to provide clearance, location, or frequent assembly and removal? | Measured size results for both mating components and a fit review based on the applicable ISO 286 tables. |
| Interference fit | Example: a permanent press fit between a shaft and a hub, where assembly force and service conditions are considered. | A fit such as H7/p6 may be considered for some applications; verify the resulting limits for the nominal size and design conditions. | Can the supplier control the mating dimensions and advise whether the specified fit is manufacturable and inspectable? | Recorded dimensions for both parts and, if specified, an assembly procedure or verification record. |
| General dimensional tolerances | Identify critical dimensions individually; use a stated general tolerance standard only for dimensions not otherwise toleranced. | Do not rely on a general tolerance to define a functional fit or a GD&T requirement. | Will the supplier flag dimensions that lack a tolerance or conflict with the stated fit and geometric controls? | Completed drawing review and first-article inspection results for designated critical dimensions. |
| Surface finish | Specify surface texture on functional surfaces such as bearing seats, sealing faces, and sliding interfaces. | State the required surface-texture parameter and value on the drawing; do not infer finish from a dimensional tolerance. | Can the supplier achieve and measure the specified finish on the actual feature and material? | Surface-roughness measurement record where required, with the parameter and measurement location identified. |
| Material and condition | Specify material grade, temper or condition, and any required heat treatment or material certification. | These requirements are separate from GD&T and dimensional fit definitions but can affect machinability and final dimensions. | Can the supplier maintain material identification and account for dimensional changes from heat treatment or finishing? | Material certificate or traceability record, plus relevant process and final-inspection documentation. |
| Inspection capability and reporting | Agree on first-article, in-process, and final inspection requirements before production begins. | Inspection must evaluate the specified dimensions, GD&T controls, and fit limits using appropriate methods. | Are calibrated instruments, trained inspectors, documented procedures, and required reporting available? | Inspection plan, calibration records, first-article report, and final dimensional report as agreed in the purchase specification. |
Fit note: ISO 286 fit symbols describe tolerance zones and grades. The actual upper and lower limits vary with nominal size, so calculate the limits using the applicable ISO 286 tables and confirm that the selected fit meets the assembly’s functional requirements.